E-mail: info@gem-cablesolution.com
 Address: No.8 Yuefeng Rd, High Tech Zone, Dongtai, Jiangsu, China | No.109 Qilin East Rd, Daning, Humen, Dongguan, Guangdong, China.
 English
 English
 русский
 日本語
 Español
 عربى
 中文简体
 Product Category

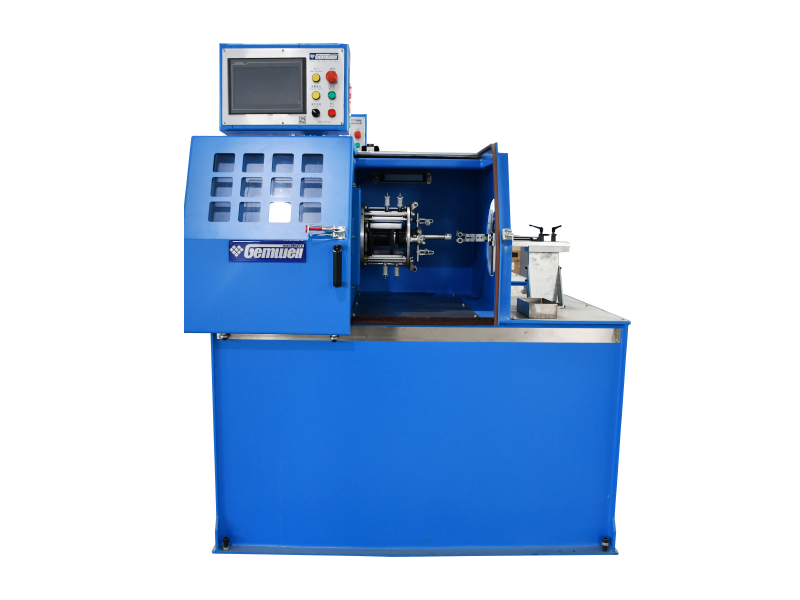
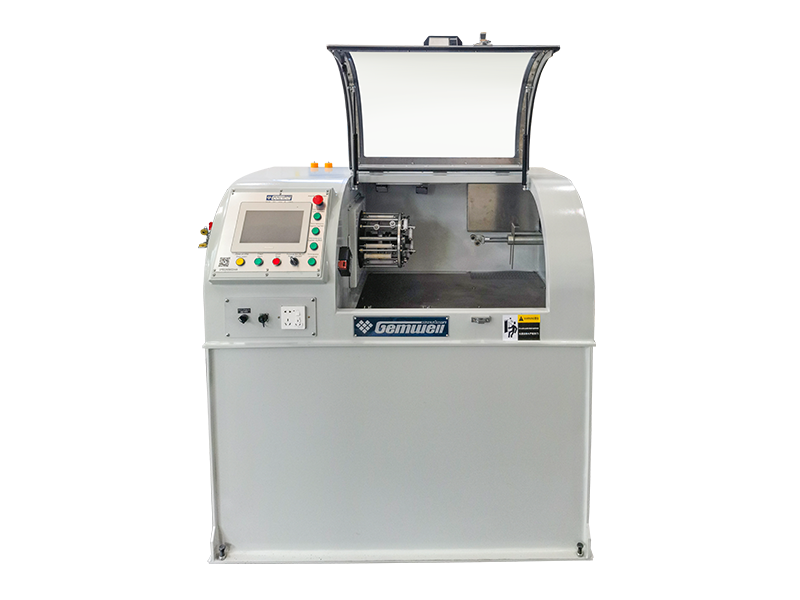
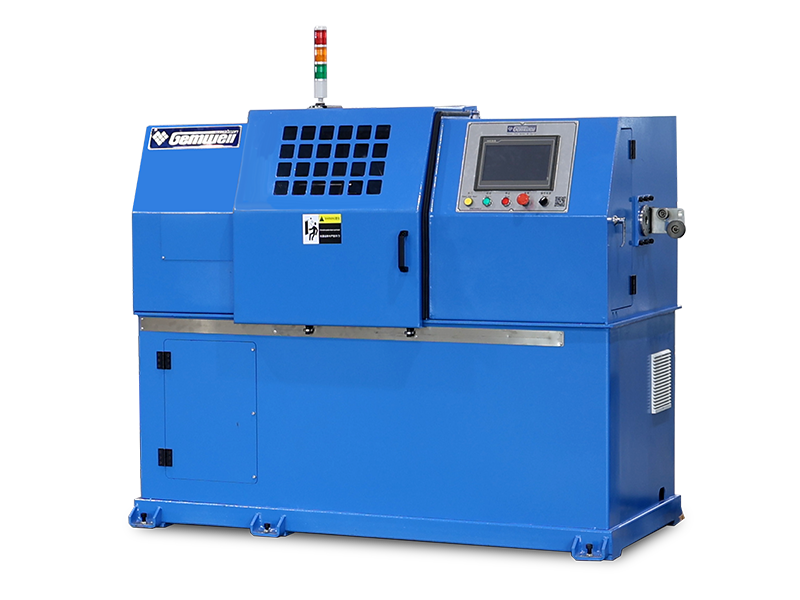
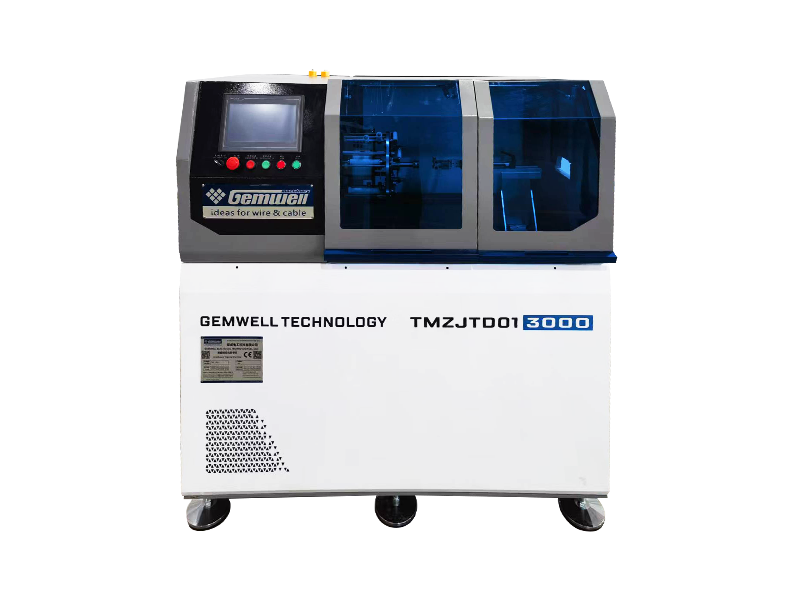
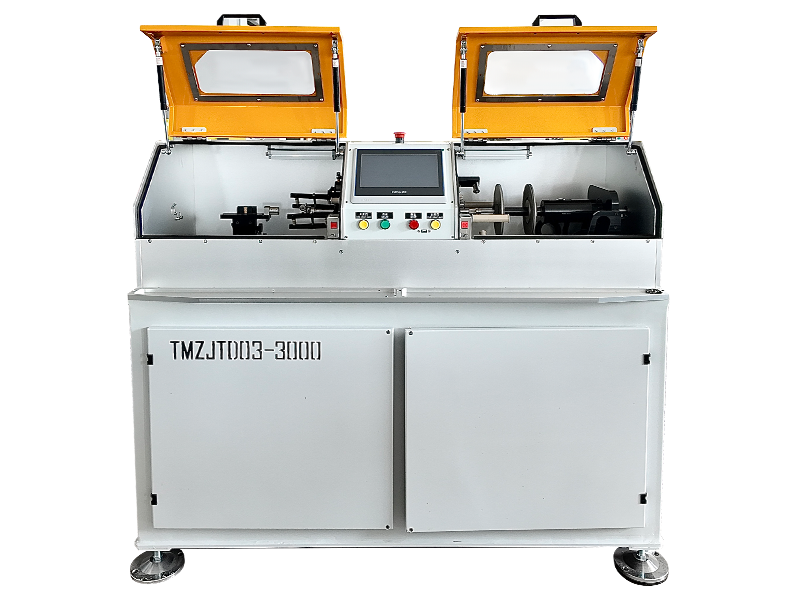
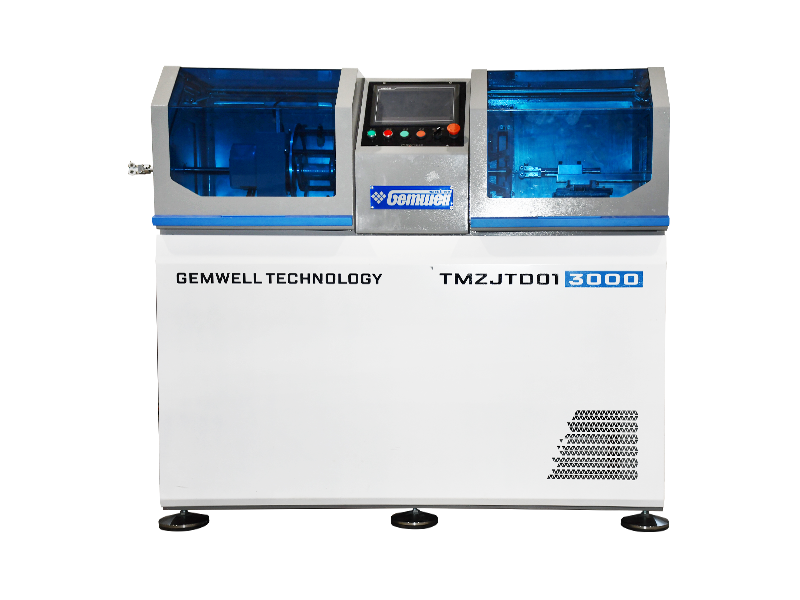
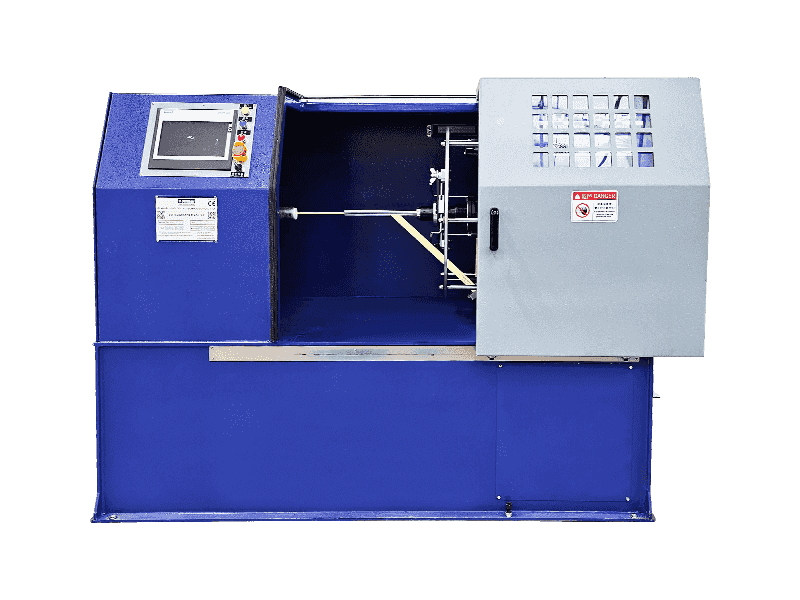
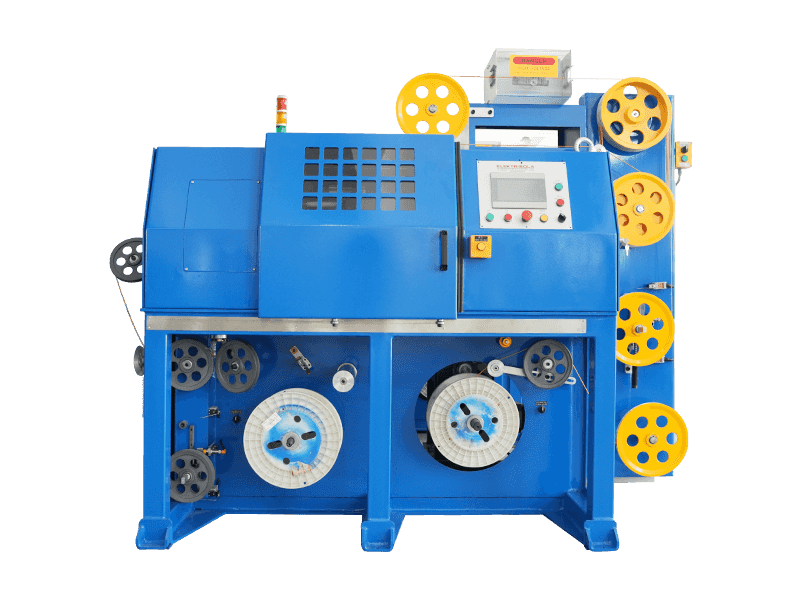
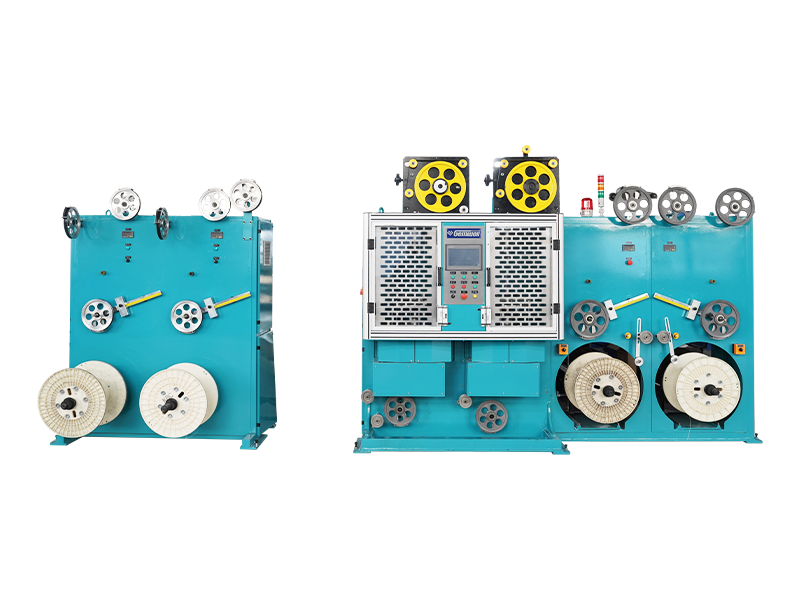
Covering the surface of wire and cable with strip materials is one of the important processes in wire production line, which has the functions of isolation, shielding, insulation, fire resistance, and temperature resistance. The wrapping methods include spiral wrapping, dragging (side) wrapping and longitudinal wrapping.
Spiral wrapping means that the core wire does not rotate while the spinning and taping head rotate concentrically around the core wire. The strip material is spirally wrapped around the core wire through the circular rotating motion of the taping head and the linear traction motion of the capstan. The wrapping angle is generally around 30-60 degrees, and the overlapping ratio can be adjusted within the range of 0-80%.
Drag (side) wrapping refers to the rotation of the core wire. The strip material is dragged in (rolled in) from the side with the rotating core wire. The wrapping angle is generally around 30-60 degrees, and the overlapping ratio can only be achieved by replacing strip materials of different widths.
Longitudinal wrapping means that neither the core wire nor the strip material rotates. The core wire and strip materials are linearly dragged by capstan at the same time, and gradually transforms the strip material into a forming package through the longitudinal wrapping mold. The wrapping angle is 90 degrees, and the overlapping ratio (generally around 5-10%) is achieved by replacing strip materials of different widths.
Commonly used taping materials include Aluminum Foil tape, Mylar tape, Copper Foil tape, Polytetrafluoroethylene tape, Mica tape, Polyimide tape, Polyester tape, etc. A general wire tape wrapping production line mainly consists of pay-off, taping head, capstan, and take-up. There are some auxiliary equipments added involved in the above process depending on the type of taping materials and detailed specifications for finished wire. The wire taping machine is available for vertical or horizontal structure. The vertical structure is suitable for small-sized cables, and the horizontal wrapping machine is more compactable with both large and small cables.
The wrapping methods include gap wrapping, butt-seam wrapping, and overlapping wrapping. Gap wrapping means that there is a certain gap between the previous and the next spiral tape edge. Butt-seam wrapping means that the edges of adjacent spiral wrapping tape are closely connected to each other. Overlapping wrapping means that when strip materials are wrapped, the previous spiral strip edge is covered by the next one. Overlapping wrapping is the commonly used method for wire and cable industry. Generally, the overlapping ratio is greater than 67% for single-layer wrapping and greater than 40% for double-layer wrapping. When double-layer or multi-layer is used, the wrapping directions should be opposite for each adjacent layer.
The wrapping process technical parameters include taping direction, pitch, angle, capstan speed, taping head rotation speed, taping tension, etc. The taping pitch refers to the distance that the wire core advances in the axial direction after one rotation by the wrapping head. The rotation speed of the wrapping process refers to the rotation speed of the taping head. The taping angle refers to the angle between the perpendicular axis of the wire movement line and the wrapping tape from taping head. The taping tension refers to the tensile force exerted at the taping point on the wrapping tape that passing through the guide wheel. The taping direction, pitch, tension, and finished outer diameter are the main parameters during the wire wrapping process, and the taping angle is the main parameter for taping machine design and manufaction. The thickness and overlapping ratio of the tape are determined based on the outer diameter of the wire core and finished wire. The width of the tape can also be determined based on the conductor outer diameter, overlapping ratio and taping angle. With a known tape width, a proper taping pitch can be selected to meet up with the overlap requirements.
The stability of the wrapping tension determines the quality and performance of the finished product. Uneven wrapping tension or unreasonable wrapping tension settings will cause defects such as uneven color, wrinkles, and “snakes” on the surface of the wire. The setting of the taping tension depends on the tensile strength of the wrapping material and the tension of the wire core. The material type, width and thickness of the wrapping material determine its tensile strength. Therefore, for different wrapping material or wire core specifications, the settings of taping tension differ.
The taping tension includes passive electromagnetic tension type and active servo tension type. The passive type uses magnetic powder clutch or hysteresis clutch as the tension element, which tracks the consumption of the outer diameter of the tap material pad or bobbin through meter or rotation counting. The electrical control system simulates the current output tension of the tension element to decrease. With this tension control method, tension is relatively stable and can basically meet the requirements of ordinary wire wrapping production in the cable industry. It has a simple structure with an economical and affordable price. The active type is divided into three-servo dancer type and capstan roller spit type. The main feature of three-servo dancer type is its tension dancer. The servo motor provides motion and tension to the tension dancer, and generates PID dynamic feedback to keep tap pay-off at a constant speed. Tension remains constant during the taping process, and it is not affected by the consumption of the outer diameter of the material tray. The capstan roller spit type doest not have a tension dancer. After the strip material is pulled out from the material tray through capstan wheel, it is immediately wrapped around the wire core. Taping tension is set according to the desired outer diameter of the finished wire. The outer diameter of the finished wire is set as a constant in the control panel, therefore, the taping tension remains constant for the whole procedure. The mechanical structures of these two active type taping machines are distinct, but both types are of great qualities. Due to the complex mechanical structure, advanced control system hardware and software configuration, the active type taping machine has a high production cost. But it can meet the stringent wrapping quality requirements in the wire and cable industry, with an effective rate close to and high cost performance. It is especially suitable for wire and cable products that require comprehensive electrical testing.
With the advancement of science and technology, taping machines must progress in the direction of high performance, high efficiency, high reliability, and high intelligence. As a explorer of new technologies of wrapping strip materials in the global wire and cable field, Gemwell Technology still focus on technology innovation and advancement. Gemwell Technology will create more high-quality Wire Taping Machine for you.

Establishment time

Building area (m²)

Number of employees

Intellectual property
A Mature Factory You Can Count On
 2026-10-26
 Webmaster
XLPE insulation exists for one reason: ordinary polyethylene cannot hold up when a cable gets hot. Cross-linking rewires the polymer structure so the
Read More +
2026-10-19
Webmaster
At the back of every router there is at least one port shaped like a wide telephone socket, and the cable that fits into it is an Ethernet cable. In
Read More +
2026-10-12
Webmaster
The Direct Answer: What You Should Expect From a Copper Wire Stranding Cross Section Machine A copper wire stranding cross section machine is judged
Read More +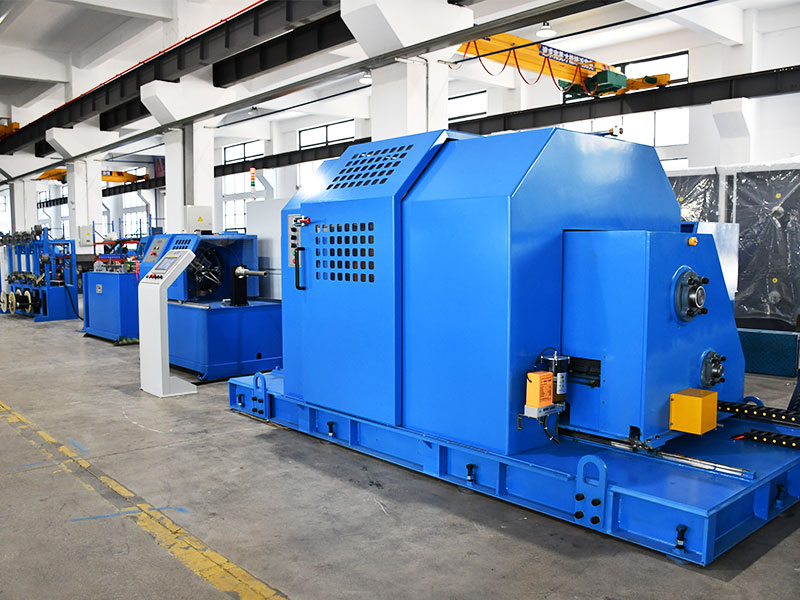
2026-10-05
Webmaster
What Is a Precision Wire Extrusion Machine? A precision wire extrusion machine is a production line that melts polymer resin, feeds it through a prec
Read More +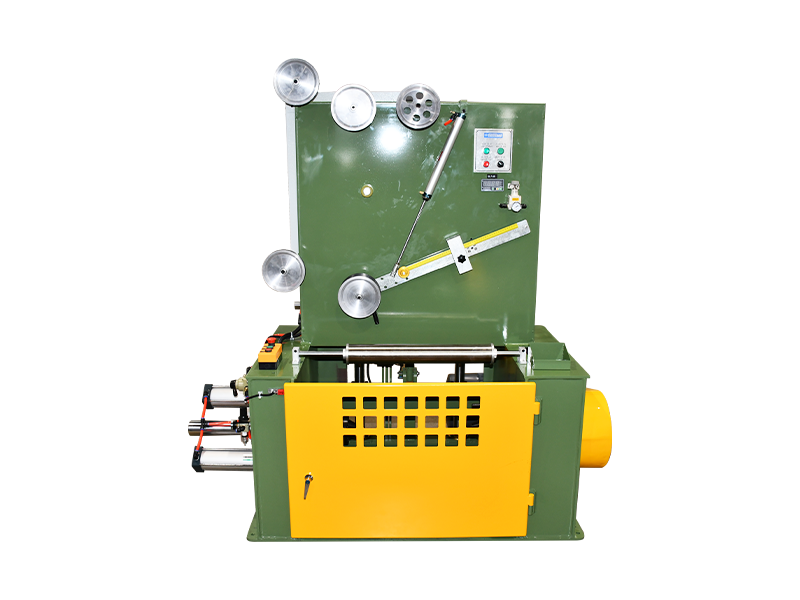
2026-09-29
Webmaster
Wire China 2026 | Successful Conclusion, A New Journey Together Watch the highlights from Wire China 2026, where industry professionals gath
Read More +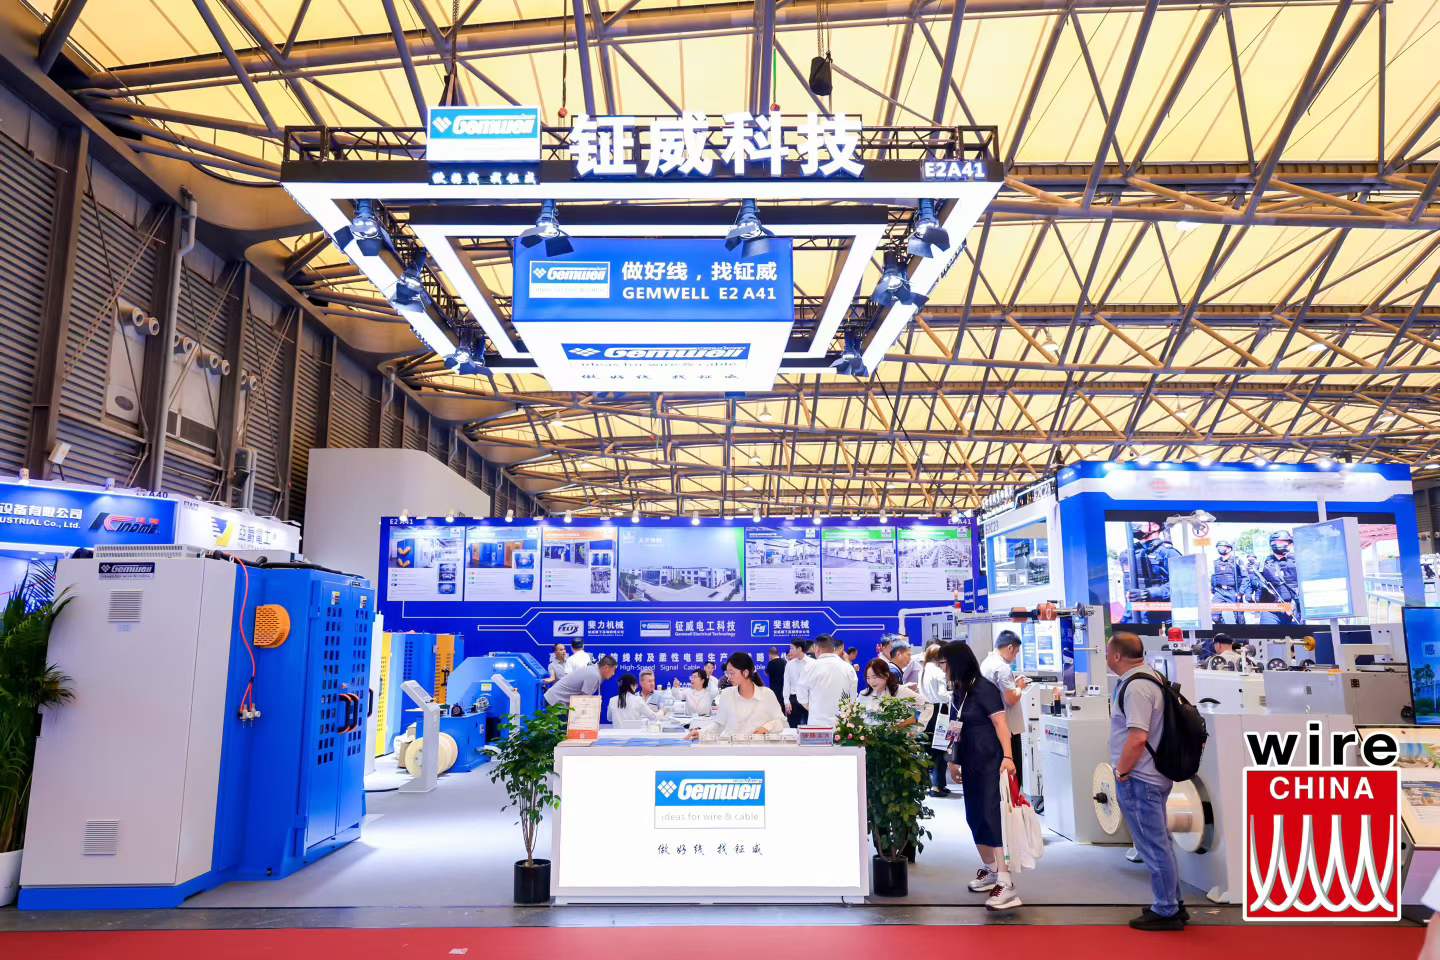
A wire taping machine wraps a thin strip of tape around a wire or cable core so the finished product picks up insulation, shielding or heat resistance that the extruded layers alone cannot give. The category runs from a compact Wire Taping Machine for fine signal wire to a complete line with pay-off, taping head, capstan and take-up. An Automatic Wire And Cable Taping Machine controls tension, pitch and line speed by itself, so the wrap laid down on the first meter matches the one on the last. Anyone comparing an automatic cable taping machine, planning wire and cable taping for a new cable type, or shopping for a tape wrapping machine runs into the same questions: which wrapping method to use, how much overlap to set, and how to keep tension steady. The sections below go through them, along with the way Gemwell Electrical Technology Co., Ltd. works with cable manufacturers on a taping project.
Every job in wire and cable taping starts with how the strip meets the core, because that choice caps the angle and the overlap you can reach. The tape layer gives the cable isolation, shielding, insulation, fire resistance or temperature resistance, depending on the material. Gemwell Electrical Technology Co., Ltd. describes three wrapping methods on its product page, and they differ more than the names suggest.
| Method | What moves | Wrapping angle | Overlap |
|---|---|---|---|
| Spiral | Core stays still, taping head rotates around it | About 30-60 degrees | Adjustable, 0-80% |
| Drag (side) | Core rotates, tape is rolled in from the side | About 30-60 degrees | Changed only by swapping tape width |
| Longitudinal | Neither moves, tape is formed around the core by a mold | 90 degrees | Around 5-10%, set by tape width |
The tapes seen most often are aluminum foil, Mylar, copper foil, polytetrafluoroethylene, mica, polyimide and polyester. They tend to sort by job:
A taping machine comes in vertical or horizontal form. The vertical structure suits small-sized cables, while the horizontal one is more compact and copes with both large and small cables. Floor space and the cable range you plan to run usually decide it.
Overlapping wrap is the method most cable plants rely on. Gemwell's rule of thumb is an overlap above 67% for a single layer and above 40% for a double layer, with adjacent layers wrapped in opposite directions. Those percentages look abstract until you turn them into layers of tape.
Each head rotation advances the core by the tape width multiplied by (1 minus the overlap). Any spot on the core is therefore covered by 1 divided by (1 minus the overlap) layers on average.
Average tape layers at each overlap ratio, calculated from the relationship above. Orange dots mark the 40% and 67% guideline values.
At 50% overlap the core carries two layers on average. At 67% it carries three, and pushing on to 80% gives five. With the same tape width and thickness, tape use per meter of cable rises with the layer count, so those last 13 points of overlap cost roughly 65% more tape. Spiral wrapping lets you dial anywhere from 0 to 80%, which is exactly why the setting deserves a deliberate choice.
The taping angle is mainly a machine design parameter. On the production floor the settings that matter are direction, pitch, tension and finished outer diameter.
Guideline overlap ratios by wrapping construction. Spiral figures are minimums, the longitudinal figure is a typical range. Source: Gemwell Wire Taping Machine product page.
This is the arithmetic that comes up early when Gemwell Electrical Technology Co., Ltd. talks a new cable type through with a customer, since cable type and production efficiency targets decide how much tape the line has to handle, and at what pitch and speed.
Tension decides whether a wrap looks clean. Uneven or badly set tension leaves uneven color, wrinkles and "snakes" on the wire surface. The right setting depends on the tensile strength of the tape and the tension of the core, and tape type, width and thickness fix that strength. Three control designs are in common use.
A magnetic powder clutch or hysteresis clutch acts as the tension element. The controller follows the shrinking tape pad by counting meters or rotations and lowers the output current to match. Tension stays fairly stable, the structure is simple and the price is friendly, which covers ordinary wrapping work. Gemwell Electrical Technology Co., Ltd. builds this design as its Hysteresis Tension Type, with models for mica wire, litz wire and high frequency wire.
Servo motors drive a tension dancer, and PID feedback keeps the tape pay-off running at a constant speed. Tension does not drift as the pad is used up. The Three Servos Active Type covers parallel pair signal wire, phase stable cable, new-energy data cable and ultra-fine wire.
There is no dancer in this design. The capstan wheel pulls tape off the pad and lays it straight onto the core. Tension is worked out from the finished outer diameter entered on the control panel and stays constant for the whole run. The Servo Spit Active Type is offered for parallel pair signal wire and ultra-fine wire.
Relative, qualitative scores (5 is best) based on the characteristics Gemwell describes for each design. They are not measured values.
Active designs cost more because of their mechanics and control hardware, but for cable that goes through comprehensive electrical testing they are the safer match. If that describes your product, an automatic cable taping machine with active tension control is the sensible place to start.
When a batch leaves the line with a wrap that looks off, the cause is usually one of a few settings. The process behind a wrap covers tape pre-assembly, tension control, winding angle calibration and end treatment, and a deviation at any of these shows up on the surface or later during electrical testing.
This is why Gemwell Electrical Technology Co., Ltd. builds a closed-loop feedback into its designs. According to its product FAQ, tension sensor data is monitored in real time and servo speed adjusts automatically to hold winding uniformity within 0.1 mm, and an automatic tape change system cuts down manual intervention during long runs.
Tape wrapping machine projects go more smoothly when the supplier has already seen a lot of production floors. Over the past 20 years, Gemwell Electrical Technology Co., Ltd. has delivered and serviced more than 10,000 pieces of equipment worldwide.
Gemwell at a glance. Source: Gemwell company information and product page (gemwellcmc.com).
By working closely with customers to develop production processes, machinery and maintenance practices, the team has built up the knowledge that sits behind its consulting services. Those services are designed to help cable manufacturers keep production line efficiency and product quality high, and the aim is to find, together with you, the solution that fits your specific needs. A project usually moves through two stages.
Detailed discussions with the customer come first, to understand requirements and project specifications: the type, scale, process flow and production efficiency of the cable equipment. In practice that means questions such as single-core or multi-core, meters per day, stand-alone or linked to other machines, and how much output per minute is targeted. Site conditions count too, since a high-humidity workshop can call for extra moisture protection.
What comes out of the needs analysis feeds the design: selecting the appropriate automation control technologies and equipment, then settling the workflow, data communication and system integration. Typical points discussed at this stage, taken from Gemwell's product FAQ:
The same FAQ quotes a few results from Gemwell's taping machines. Read them as company-reported figures, not independent test data.
Company-reported figures from the Gemwell Wire Taping Machine FAQ (gemwellcmc.com). The lighter segment marks the upper part of the 20-30% range.
Gemwell's rule of thumb is above 67% for a single layer and above 40% for a double layer, with the two layers wrapped in opposite directions. Longitudinal wrapping sits much lower, around 5-10%, and is set by tape width.
Passive control is simple and affordable and handles ordinary wrapping well. Active control, whether three-servo dancer or capstan spit, costs more but suits products that need comprehensive electrical testing and tight wrapping quality.
Cable type, cable diameter range, daily output, tape material and width, whether the machine stands alone or joins an existing line, and the efficiency you are aiming for. These are the same points Gemwell Electrical Technology Co., Ltd. works through in its needs analysis.
Yes. Gemwell's FAQ describes industrial Ethernet or Modbus links to a higher-level system for tension deviation and production statistics, OPC UA for large plants, and simpler interfaces where a lighter setup is enough.
Servicing is part of the work. With more than 10,000 pieces of equipment delivered and serviced over 20 years, Gemwell also advises on production processes and maintenance practices so the line keeps its efficiency and product quality.
 Custom Wire Taping Machine Manufacturers